Connection and measuring points for passive PROFINET diagnostics
TAP measuring points for passive PROFINET diagnostics
We recommend installing the permanent TAP connection point directly behind the PLC (IO Controller), between the control system and the rest of the PROFINET network. A technician can then connect to the prepared measuring point at any time, even while the production line is running at full operation, and start passive diagnostics without disconnecting the PROFINET communication.
A portable TAP adapter or a NODKA industrial PC with PNT PROFINET Tool installed can be connected to the measuring point. The PC is connected to the two monitoring ports of the TAP connection point using two Ethernet cables and monitors both directions of communication. This allows the technician to evaluate cyclic communication, alarm and diagnostic messages, and the current PROFINET network load.
Choose the measuring point by network speed and manufacturer
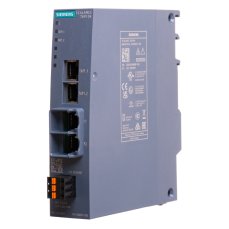
SCALANCE TAP104
Permanent SIEMENS measuring point for passive diagnostics of PROFINET communication at 100 Mbit/s.
View SCALANCE TAP104EtherMIRROR 100M
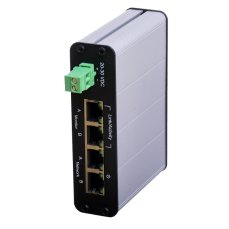
Permanent plug & play measuring point for passive diagnostics of standard 100 Mbit/s PROFINET networks.
View EtherMIRROR 100MEtherMIRROR 1G
Measuring point for passive communication analysis at speeds of up to 1 Gbit/s. Suitable for gigabit sections of an industrial network.
View EtherMIRROR 1GWe will check the network speed and topology and recommend a measuring point, TAP adapter or a PNT Tool solution with a NODKA PC.
In detail: what a TAP measuring point is used for and how to choose one
Passive diagnostics while the production line is running
We recommend permanently installing the TAP measuring point directly behind the PLC (IO Controller). This position allows communication between the control system and the downstream part of the PROFINET network to be monitored. During diagnostics, the technician simply connects to the prepared monitoring ports without disconnecting the live communication path or stopping the production line.
A portable TAP adapter or a NODKA industrial PC with PNT PROFINET Tool installed can be connected to the monitoring ports. The PC’s two Ethernet interfaces are connected to the measuring point using two cables. The software then passively monitors both directions of communication and evaluates communication cycles, alarm and diagnostic messages, and network load.
The TAP measuring point is permanently installed between the PLC and the downstream part of the PROFINET network.
The technician connects a TAP adapter or NODKA industrial PC to the monitoring ports using two Ethernet cables.
PNT Tool or another analyzer monitors communication cycles, alarms, diagnostic messages, timing and network load.
Comparison of measuring points
| Product | Network speed | Typical application | Selection |
|---|---|---|---|
| SIEMENS SCALANCE TAP104 | 100 Mbit/s | PROFINET networks where the customer prefers an original SIEMENS solution | View product |
| EtherMIRROR 100M | 100 Mbit/s | Standard PROFINET networks, preventive measurements and permanent connection of diagnostics | View product |
| EtherMIRROR 1G | 1 Gbit/s | Gigabit sections of industrial networks and communication using eight-core cables of at least Cat5e | View product |
Frequently asked questions about PROFINET measuring points
In the switch configuration, set communication mirroring from the port connected to the PLC to the laptop port. PNT Tool can then display the PROFINET data exchange rate, cyclic communication, network load, and alarm and diagnostic messages.
However, a mirrored port cannot correctly measure PROFINET communication jitter. A TAP adapter installed in the communication path is required to measure jitter.
Send us the network topology, its speed and the required diagnostic method. We will recommend the measuring point location, a suitable TAP adapter, measurement via a mirrored port or a permanent PNT PROFINET Tool solution with a NODKA industrial PC.
Scalance TAP104
EtherMIRROR 100M
742,94 EUR Incl. VAT
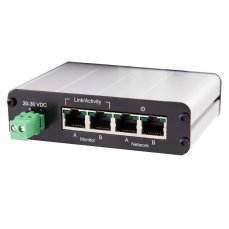
EtherMIRROR 1G
2 087,25 EUR Incl. VAT
From Practice: At De & Co, They Can Find a PROFINET Fault in Just a Few Minutes
De & Co Hranice s.r.o. supplies production lines and robotic workstations for various industrial sectors. As the company gradually moved from smaller machines to large automated lines, the complexity of its communication networks increased as well. This created a need to diagnose PROFINET and at the same time connect securely and remotely to equipment already operating at customer sites. What technologies help their technicians do that?
The 3 Biggest Killers of the PROFINET Industrial Network
Our engineers perform diagnostics of industrial networks in hundreds of manufacturing companies. They travel across the country to find the causes of failures. We have asked them what problems they have most frequently diagnosed in customers' PROFINET networks recently. What have they told us?
We train the basics and troubleshooting of PROFINET networks | FOXON Academy
Do you know how the PROFINET industrial network works? Do you know how to find errors that can cause it to drop out? Do you regularly check the condition of the cabling and connectors? You can learn everything in a two-day training course full of practical examples.
Which switch for PROFINET networks?
Is it advisable to use cheap unmanageable switches for a few crowns or is it worth paying extra and buying manageable switches? Should I save money on buying switches for the production line or should I buy a quality PROFINET switch?
Question or Inquiry
Highlighted items are mandatory.